

Manual vs. Automated Visual Inspection: 7 Risks of Manual Inspection in Pharma
If you are responsible for quality assurance or production in pharmaceutical manufacturing, you have probably asked yourself this question more than once: Why should we automate our visual inspection when trained inspectors have been doing this job reliably for years? Whether the challenge comes from management asking about costs, or from an auditor who wants to know why manual inspection alone is considered sufficient – you need solid arguments, not a gut feeling.
That is exactly what this article delivers: the seven structural risks of manual visual inspection in pharma, a direct manual vs. automated comparison, the regulatory perspective on data integrity, and a checklist with seven questions for your automation decision. If you want to know what this means concretely on your line – from the most common tablet defects such as capping, chipping, or mottling to subtle color deviations that the eye misses – read on.
Why manual visual inspection is still the standard in pharma
Manual visual inspection has a long tradition in the pharmaceutical industry – and for good reasons. It is flexible, requires no investment in inspection technology, and human inspectors can react to unexpected situations without any retooling. GMP explicitly permits manual inspection – many companies have been operating in compliance for decades with trained, qualified visual inspectors.
But the environment has changed. Expectations for 100% inspection of tablets have risen significantly – driven by complaints, recalls, and stricter audit findings. At the same time, data integrity has become a central audit topic: authorities want to know not only that a product was inspected, but also how, when, by whom, and with what result – documented in a tamper-proof manner. Both developments put manual visual inspection under pressure, because the weaknesses of the human inspector are not a question of qualification or discipline. They are structural.
The 7 risks of manual visual inspection
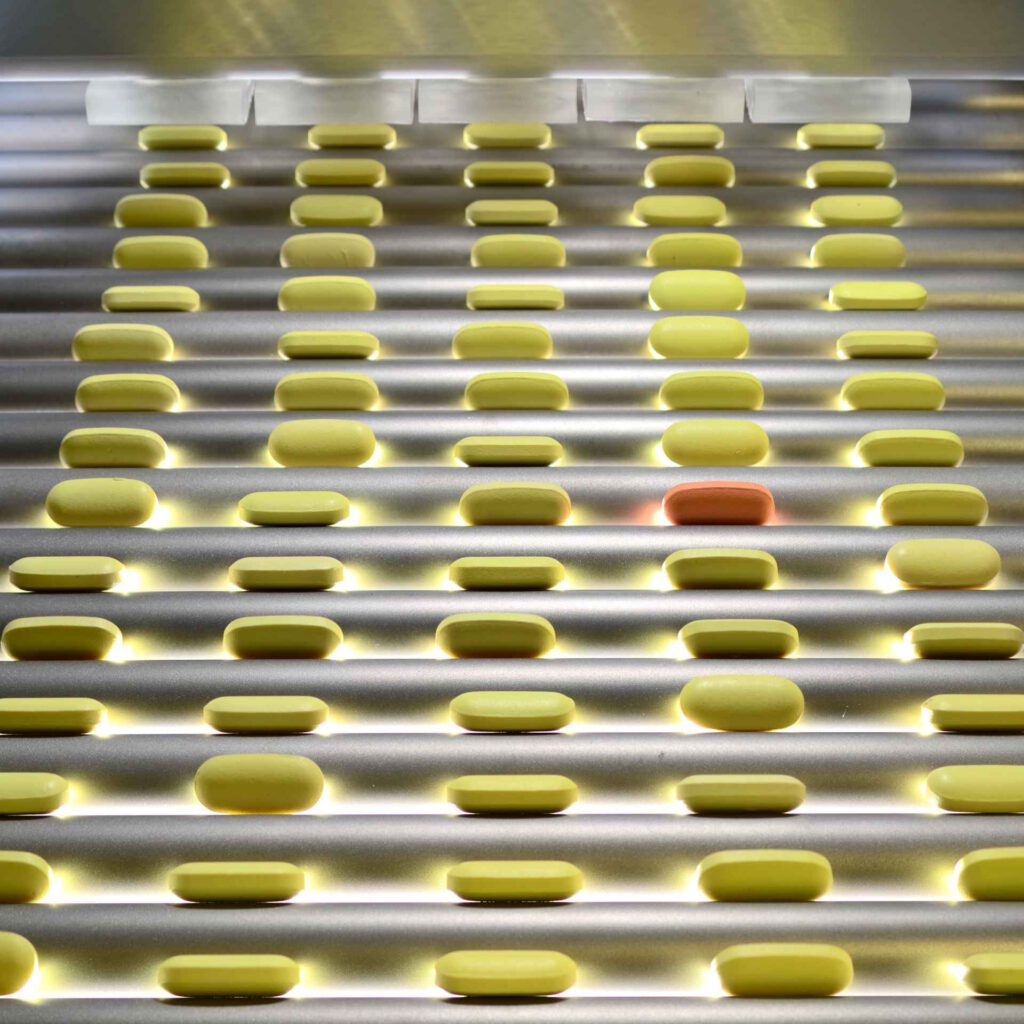
The following seven risks apply regardless of how experienced your visual inspection team is. They are rooted in human physiology and organizational reality – and that is exactly why they are such strong arguments in discussions with management and auditors.
Risk 1: Attention is a finite resource
Concentration on monotonous visual inspection tasks measurably declines over time – a well-established finding of occupational psychology. Visual inspection, personnel, fatigue: an inspector who examines thousands of visually similar units per hour cannot bring the same attention at the end of a shift as at the beginning. The practical consequence: detection performance fluctuates within a shift, between shifts, and during peak loads. Rotation schedules and break regimes mitigate the effect but cannot eliminate it.
Risk 2: Sensitivity decreases with speed
The reliability of manual inspection is inversely proportional to throughput. The faster products pass the inspector, the more defects go undetected – a classic speed-accuracy trade-off. Practical consequence: during high-load phases, staff shortages, or at the end of a campaign, inspection quality is at its lowest precisely when the volume at risk is greatest. An automated system, by contrast, applies the same sensitivity at any qualified speed.
Risk 3: The resolution limit of the human eye
The human eye has a physical resolution limit, and manual visual inspection typically works only with diffuse workplace lighting. Fine cracks, small edge chips, slight mottling, or subtle coating defects lie below what an inspector can reliably detect – especially at production speed. Camera-based systems overcome this in two ways: through higher optical resolution and – equally important – through targeted lighting. Dedicated lighting arrangements (such as directional light that makes surface structures cast shadows, or transmitted light for transparency checks) make defect classes visible that simply do not appear under diffuse light. That is a core strength of an automatic visual inspection system: cameras reliably detect smaller defects than the eye – without any loss of speed.
Risk 4: No two inspectors judge alike
Visual inspection involves discretionary decisions – and discretion varies from person to person. What one inspector classifies as an acceptable cosmetic deviation, another rejects. This inter-inspector variance is a known challenge in GMP visual inspection: borderline cases are decided inconsistently across shifts, sites, and even by the same person over time. Practical consequence: the same batch can pass or fail – depending on who inspected it. An automated system applies an objective, validated decision criterion to every unit – reproducibly, around the clock.
Risk 5: Documentation gaps and data integrity
Manual inspection is traditionally documented manually: tally sheets, counters, handwritten records. This creates two problems. First, the documentation effort per batch is considerable and error-prone. Second, manual records cannot prove what was actually seen – only what was written down. In an audit, the question “How do you ensure that every unit was actually inspected?” can hardly be answered convincingly with paper records: no automatic audit trail, no electronic reject log, no image evidence. We cover the regulatory dimension of this point in the next section.
Risk 6: Throughput does not scale
The capacity of manual inspection scales linearly with personnel: more tablets per hour mean more inspectors, more workstations, more shifts. Every increase in batch size drives inspection costs and organizational complexity directly upward – hiring, qualification, shift scheduling, substitution arrangements. Practical consequence: manual visual inspection becomes a bottleneck and a permanent cost driver – exactly where production wants to grow. Where inspection takes place directly in the material flow – such as counting machine inspection (CountSecure360) – an automated unit inspects at full line speed without additional personnel.
Risk 7: Training and requalification effort
Qualified visual inspectors are not available off the shelf. Initial qualification, regular requalification with defect-sample sets, vision tests, and documented training tie up considerable QA and HR resources. Staff turnover makes this a permanent cycle: every new inspector starts the effort from scratch, and every gap in requalification records is a potential audit finding. An automated system must also be qualified and validated – but once validated, it works identically every day, and requalification follows controlled change management instead of personnel availability.
By the way: All 7 risks can be addressed structurally – TabletSecure360° inspects every single tablet by camera, ejects defective products with full documentation, and records every decision in an audit-proof manner. And for retrofitting directly at the counting machine (e.g., Cremer, Swiftpack) there is CountSecure with single-product ejection.
Manual vs. automated visual inspection – the direct comparison
The following table summarizes the key criteria. The cost column is deliberately kept qualitative: absolute figures depend on your line, batch sizes, and defect profile – the relevant question is *which* cost drivers dominate.
Criterion | Manual inspection | Automated visual inspection |
|---|---|---|
Detection sensitivity | Limited by the resolution of the human eye; fine cracks, small edge chips, and subtle color deviations are unreliable | Camera resolution and image processing reliably detect smaller defects; sensitivity is defined and validated per recipe |
Throughput per hour | Limited per inspector; scales only via additional personnel and workstations | Inspects at full line speed; capacity scales with the machine, not with headcount |
Lighting | Typically only diffuse workplace light | Targeted lighting arrangements (directional, diffuse, transmitted light), matched to each defect class and product |
Documentation / audit trail | Manual tally sheets, counters, and records; no image evidence; error-prone | Automatic recording of results, reject counts, and images; electronic audit trail per batch |
An honest note: automated inspection is not the answer in every situation. Very small batches, highly variable product mixes with frequent changeovers, or niche dosage forms can justify semi-automated inspection or a manual process with strong controls. The checklist below helps you decide where your line stands.
End fatigue and sampling – TabletSecure360° makes your visual inspection audit-proof
Replace error-prone manual inspection with a **documented 100% camera inspection**: every tablet is inspected individually, every ejection is recorded in an audit-proof manner – exactly the data integrity auditors ask about.
- **100% inspection with no fatigue curve** – constant detection performance, shift after shift
- **Up to 700,000 products per hour** – throughput scales with your line instead of your personnel
- Documentation – management:** batch record, audit trail, 4-level password structure, recipe management, gapless reject logging
The regulatory perspective – data integrity and auditability
Data integrity has become one of the most prominent topics in GMP inspections worldwide. The widely used **ALCOA+ principles** require that quality-relevant data be attributable, legible, contemporaneous, original, and accurate – complemented by complete, consistent, enduring, and available.
Applied to visual inspection, purely manual processes face an uncomfortable situation:
- **Attributable:** Who inspected which unit? With manual inspection, attribution exists at best at batch level – never at unit level.
- **Contemporaneous and original:** Results are recorded after the fact, on paper or counters – not at the moment of the inspection decision.
- **Complete and available:** There is no evidence of what was *seen* – no images, no reject log per unit, nothing that could be retrieved years later during a complaint investigation.
Automated 100% visual inspection with an electronic audit trail addresses these points structurally. Every unit is inspected, every reject decision is recorded with a timestamp and typically image evidence, and the data resides in a controlled, tamper-proof system. That is also why requirements for electronic records and signatures – commonly referenced via FDA 21 CFR Part 11 in the USA and Annex 11 of the EU GMP Guide in Europe – are most naturally met by validated automated systems rather than paper-based manual documentation.
The authorities do not prohibit manual inspection. But auditors increasingly ask how a company ensures inspection reliability and data integrity with manual processes alone. Pointing to an automated 100% inspection with a complete audit trail turns a difficult audit discussion into a short one. That is exactly why TabletSecure360° records every inspection decision and every ejection with an image – including user management and audit trail – batch record.
When does automation pay off? – Checklist with 7 questions
Use the following seven questions as a decision framework – and as a basis for discussion with your management. The more questions you answer with “yes,” the stronger the factual case for automating your visual inspection.
Automation decision checklist
- **Complaint history:** Have you had customer complaints or internal deviations related to visual defects in the last 24 months?
- **Defect size:** Are your critical defects (cracks, edge chips, spots, printing defects) at or below the reliable resolution limit of the human eye?
- **Throughput:** Does manual inspection limit your line speed, or does inspection quality decline as output increases?
- **Personnel:** Do you tie up significant qualified personnel in visual inspection, and do staff shortages or turnover create coverage risks?
- **Documentation effort:** Is batch documentation of manual inspection time-consuming, and are records incomplete or hard to find?
- **Audit experience:** Have auditors asked how you ensure inspection reliability and data integrity of your manual process?
- **Product variety:** Do you run multiple products where consistent, recipe-based inspection criteria would reduce changeover and training effort?
**Three or more “yes” answers** suggest that manual visual inspection is probably the weakest link in your quality control – and that the automation discussion should move from “whether” to “how and when.”
The most pragmatic next step: bring these 7 answers to a no-obligation demo with your own products – we inspect your tablets on TabletSecure360° and you get the answer to the “how” based on your real defect profile. For those who first want to upgrade only the counting machine: CountSecure retrofits existing counting lines with camera inspection.
FAQ
What does 100% visual inspection mean in pharma?
100% visual inspection means that every single unit of a batch – every tablet, capsule, or container – is visually inspected for defects instead of relying on samples. It can be performed manually by trained visual inspectors, semi-automatically, or fully automatically by camera-based systems. Regulatory expectations are increasingly moving toward documented 100% inspection for critical dosage forms.
Is manual visual inspection GMP-compliant?
Yes, manual visual inspection is permissible under GMP, provided it is performed by qualified, trained inspectors under defined and controlled conditions with appropriate documentation. In practice, however, compliance depends heavily on the robustness of qualification, requalification, and record-keeping – and auditors increasingly scrutinize the inspection reliability and data integrity of manual processes.
Which defects can human inspectors not reliably detect?
Defects at or below the resolution limit of the human eye are the classic blind spot: fine hairline cracks, small edge chips, subtle mottling, and slight color or coating deviations. Detection also becomes unreliable for defects that are only visible under special lighting conditions, and generally when inspection speed increases or the inspector’s attention declines.
What is the difference between semi-automated and fully automated inspection?
In semi-automated inspection, machines take over product transport and presentation – such as rotating the tablets in front of the inspector – while the accept/reject decision remains human. Fully automated inspection uses cameras and image processing to make the decision itself, applies validated criteria to every unit at line speed, and documents every result electronically.
When does automated visual inspection pay off?
There is no universal break-even figure; the economics depend on batch sizes, throughput, defect risk, complaint history, and personnel costs. As a rule of thumb: the higher your throughput, the smaller your critical defects, and the greater your documentation and audit pressure, the faster automation pays for itself. The checklist above is a practical starting point.
Conclusion
Manual inspection is not a relic – it is a legitimate, GMP-permissible method. But its seven structural risks do not disappear through better training or more discipline. They are properties of the method itself.
The decisive shift is both regulatory and economic: expectations for 100% inspection and data integrity are rising continuously, while automated systems deliver reproducible sensitivity, complete audit trails, and throughput that scales with your production rather than your headcount. If your checklist answers point toward automation, the logical next step is to understand how 360° inspection solves these risks – by capturing every surface of every tablet, not just the visible side.
See TabletSecure360° on your line.
Would you like to see how automated 360° visual inspection performs with your actual products – your tablets, your defect types, your line speed? Request a free, no-obligation demo of TabletSecure360° and bring the 7-question checklist along as the agenda for the conversation.